
What Should a Battery Pack Line Supplier Provide for Cylindrical Cell Assembly?
Use this checklist to clarify component scope, service boundaries, delivery expectations, and the questions that belong in a supplier review.
Read the article →Cylindrical cell front-end automation
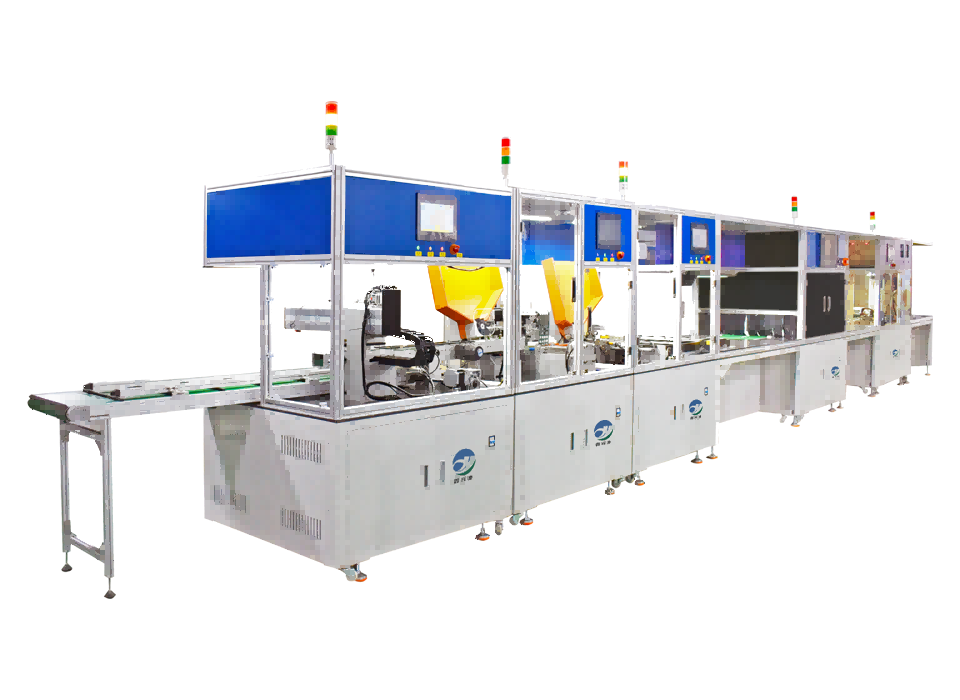
Cheebo’s single-sided automatic spot-welding system brings feeding, sorting, labeling, welding, and front-end pack assembly into one coordinated workflow. Use the battery pack production line and battery pack assembly line as a starting point for reviewing cell formats, station scope, and production targets.
From incoming cells to welded packs
The line is organized around the material decisions that affect downstream welding: how cells enter, how they are grouped, how insulation is handled, and how the finished assembly is checked.
Whole-box loading and forward feeding move cylindrical cells into the line while reducing unnecessary handling.
Multi-gear sorting helps group cells by the specifications selected for the pack design.
Labeling and insulation operations prepare the cell shoulder and terminal area before welding.
Automatic single-sided spot welding and a fixture-flipping mechanism support repeatable access to the pack.
CCD sensing provides an in-line inspection point for the configured welding and assembly process.
Product fit
The equipment is suited to cylindrical steel-shell cells used in pack assembly. The current product description lists 18650, 18700, 21650, 21700, 26650, 32650, and 32700 formats, with certain modules selected separately.
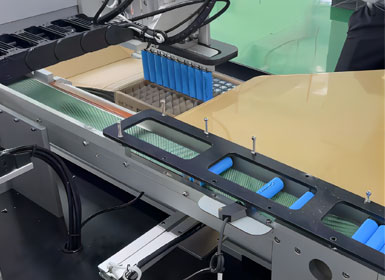
Cell presentation, sorting, and insulation are not separate from welding quality. They determine how consistently the fixture receives material and how clearly the inspection station can read the configured process.
Technical planning
Treat these values as a starting point for confirming cell dimensions, pack architecture, optional modules, and the final workstation layout.
| Planning item | Published specification | What to confirm for your line |
|---|---|---|
| Supported cylindrical cells | 18650 / 18700 / 21650 / 21700 / 26650 / 32650 / 32700 | Cell shell, terminal arrangement, pack recipe, and module selection |
| Whole-line efficiency | 3000 PCS/hour | Whether the target refers to the full configured line or a specific station |
| Operators | 3–4 for front-end assembly | Manual workstation duties and staffing at the required production rate |
| Welding motion | 350 × 600 mm XY stroke; 0.1 mm XY accuracy | Pack dimensions, fixture envelope, and weld pattern |
| Inspection | 1000W CCD pixel specification; 500 × 600 mm CCD testing scope | Inspection points, lighting, and the acceptance criteria for your product |
| Power | Single-phase 220V, 50/60Hz | Plant power, safety provisions, and final electrical configuration |
Where the line fits
The same front-end logic can be reviewed against different pack programs, provided the cell format, recipe, and station requirements are confirmed before ordering.
Single-sided welding and cell-format flexibility support front-end planning for cylindrical packs used in electric tools.
Feeding, sorting, labeling, and inspection can be considered together when a compact pack program needs a controlled input flow.
Larger cylindrical-cell programs can be assessed against the published stroke, sorting, inspection, and staffing parameters.
Further reading
These Cheebo articles add practical context for comparing supplier scope, front-end sequencing, and the preparation work that precedes spot welding.
Use this checklist to clarify component scope, service boundaries, delivery expectations, and the questions that belong in a supplier review.
Read the article →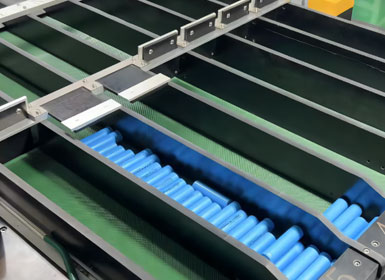
Follow the sequence from cell input to pack preparation and see which handoffs deserve attention during line planning.
Read the article →
See how cell grouping and insulation preparation shape the consistency of the material reaching the welding station.
Read the article →Common planning questions
Start with the published configuration, then confirm the exact cell and pack requirements with Cheebo.
The product description lists 18650, 18700, 21650, 21700, 26650, 32650, and 32700 cylindrical steel-shell cells. Confirm the final cell and module combination before ordering.
The described workflow combines feeding, labeling, sorting, single-sided spot welding, and front-end pack assembly, with CCD inspection included in the technical configuration.
The published technical parameters list whole-line production efficiency at 3000 PCS/hour. The applicable rate should be confirmed against the selected cell format, recipe, and configured stations.
The product information states that 3–4 people can complete the front-end battery-pack assembly workflow. Staffing should be reviewed together with the manual workstation and target output.
The listed figures include a 350 × 600 mm XY welding stroke, 0.1 mm XY-axis accuracy, a 1000W CCD pixel specification, and a 500 × 600 mm CCD testing scope.
Cheebo presents equipment customization and upgrade consultation as part of the product offer. Discuss pack dimensions, optional scanning or resistance-testing modules, and the required line layout before finalizing scope.
Share the cell format, pack arrangement, expected output, and inspection requirements so the proposed configuration can be matched to the workstations you actually need.
Cheebo Technology · Service hotline: 19928807536